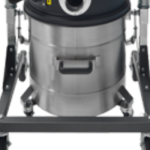



4.8 HP

26 gal
The CLEAN OIL T industrial vacuum is specifically designed to effectively vacuum and separate oil and swarf from tanks, machine tool tables, and guides. It utilizes a side-channel turbine to generate suction, ensuring exceptional speed and power. With its compact size, the CLEAN OIL vacuum can be easily maneuvered even in narrow spaces, making it highly convenient.
The vacuum cleaner’s container is equipped with a metal basket to separate the solid particles from the liquid component. Additionally, it features a 150-micron nylon filter that enhances the filtration process, ensuring optimal effectiveness.
To prevent overflow, the vacuum cleaner is equipped with a floating level switch that automatically stops suction when the container reaches its maximum capacity (capable of holding 26 liquid gallons of emulsified oil). The container is equipped with a level indicator on its exterior, allowing the operator to monitor the liquid level inside the machine.
For discharge, the CLEAN OIL T vacuum utilizes a “reverse flow” system that allows gravity to facilitate the drainage process. This system ensures that all the vacuumed and filtered lubricant-coolant is replenished within the machine, contributing to its efficient operation.

The CLEAN OIL T uses a side channel blower to deliver strong suction for coolant, oil, swarf, and light sludge recovery. Its compact design makes it easier to position near machine tools, tanks, and guides where larger sump vacuums are less practical.

The gathered liquid passes through a PPL filter with a 150µ efficiency, which enables the separation of even the tiniest solid particles. This process ensures that the filtered liquid becomes suitable for reuse. The filter is designed to be easily washed and reused. Additionally, there is an alternative disposable TNT filter with a 100µ efficiency that is also available.

A convenient lever, positioned at the rear of the vacuum cleaner, enables quick switching between vacuuming and discharging modes. The flow inversion system cleverly utilizes the exhaust air from the turbine, ensuring efficient and speedy operation.

The robust metal cyclone is equipped with a tangential inlet nozzle that effectively directs the material towards the collection bin. Within the collection bin, a float level indicator is strategically placed, which automatically interrupts the intake process by closing the cyclone when the bin reaches its full capacity. This mechanism halts the vacuuming operation, ensuring efficient and timely maintenance of the equipment.
Get answers about using the CLEAN OIL T for CNC sump cleaning, coolant and cutting-oil recovery, metal chip and swarf separation, liquid filtration, reverse-flow discharge, continuous-duty suction, and choosing the right sump vacuum for machine-tool maintenance.
The CLEAN OIL T is a three-phase industrial sump vacuum designed for recovering coolant or cutting oil together with metal chips, swarf, fines, and light sludge from CNC machines and other machine-tool tanks.
A side-channel blower provides continuous-duty suction, with the current U.S. product page listing up to 247 CFM of airflow and 100 inH2O of vacuum through a 2-inch inlet.
The machine provides 26 gallons of liquid capacity and 13 gallons of solids capacity. A metal separation basket and liquid-filtration stage help separate chips and swarf from the recovered coolant or cutting oil during sump cleanout.
The CLEAN OIL T is particularly useful for recurring machine-tool maintenance where a facility has 480 V three-phase power and wants continuous-duty suction combined with fast reverse-flow discharge of recovered liquid.
Yes. Mixed liquid-and-solid recovery is one of the primary applications of the CLEAN OIL T.
The vacuum can recover coolant or cutting oil containing metal chips, swarf, fines, and light settled sludge from CNC sumps, machine-tool tanks, tables, and guides.
A metal separation basket captures larger chips and swarf while recovered liquid passes through the filtration stage into the collection tank. This allows maintenance teams to remove the mixed contents of a machine sump in one cleanup process instead of separately pumping liquid and manually removing chips.
The application should still be reviewed when the sump contains unusually heavy sludge, extremely fine metallic particles, reactive material, flammable liquids or vapors, hot fluid, or other hazardous contaminants.
The CLEAN OIL T separates recovered solids and liquid during the same sump-cleaning process.
A tangential inlet and internal cyclone help direct incoming material toward the collection area. Larger metal chips and swarf are retained by the metal separation basket, while the recovered coolant or cutting oil passes through a washable 150 µm liquid filter.
A floating level system automatically interrupts suction when the liquid reaches the maximum operating level, helping prevent overfilling.
For discharge, the CLEAN OIL T uses a reverse-flow system. A control lever switches the machine from vacuuming to discharge mode, allowing exhaust air from the side-channel blower to help push the recovered and filtered liquid out of the tank.
This can make it faster to transfer recovered coolant back to a machine or another suitable container compared with a gravity-only discharge system.
The 150 µm filtration stage removes bulk contamination but should not be treated as complete coolant conditioning. Coolant concentration, bacteria, tramp oil, very fine particles, and other fluid-quality conditions should still be checked before reuse.
Choose the CLEAN OIL T when continuous-duty three-phase suction and fast reverse-flow liquid discharge are important. Choose the M100 OIL when a 110 V single-phase machine with simpler gravity discharge is better suited to the facility and maintenance workflow.
Both machines provide 26 gallons of liquid capacity and 13 gallons of solids capacity and are designed for coolant, cutting-oil, chip, and swarf recovery.
The CLEAN OIL T uses a side-channel blower and 480 V three-phase power. Its reverse-flow system uses blower exhaust air to discharge recovered liquid.
The M100 OIL uses three bypass motors on 110 V single-phase power and provides up to 326 CFM and 98 inH2O, with gravity as its standard liquid-discharge method.
The better choice therefore depends less on tank capacity and more on available electrical service, required duty cycle, suction characteristics, and whether gravity or powered reverse-flow discharge better fits the coolant-maintenance process.
The CLEAN OIL T may not be the best choice when 480 V three-phase power is unavailable, when the machine sump contains substantially more liquid than its 26-gallon capacity can handle efficiently, or when the application requires larger solids capacity or dedicated high-volume pump-out.
For smaller machine tanks where portability and standard 120 V power are more important, a compact single-phase sump vacuum such as the M 70 OIL may be more practical.
For larger sumps, multiple-machine maintenance routes, higher liquid volumes, or applications centered around powered liquid transfer, a larger RAM OIL or other pump-equipped sump vacuum may provide a more efficient workflow.
The CLEAN OIL T should also not automatically be assumed suitable for flammable liquids or vapors, reactive chemicals, hot fluids, unknown hazardous mixtures, or hazardous classified locations.
Final selection should consider sump capacity, chip and sludge volume, fluid chemistry, temperature, flash point where applicable, available electrical service, hose run, required pickup rate, discharge workflow, coolant-reuse requirements, and operating environment.