- (737) 320-9102


2 kW | 2.7 HP

34 gal
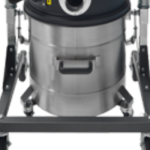
The M130 P industrial sump vacuum is engineered to efficiently collect and separate coolant and chips from tanks, worktables, and machine tools. It features a built-in pump that allows for the simultaneous suction and discharge of filtered liquids.
Recovers and recycles cutting and lubricating coolants
Streamlines coolant collection and chip removal
Enables simultaneous liquid suction and discharge
Durable powder-coated steel construction

The suction power of the vacuum is produced by two by-pass motors. Each motor has its own switch, allowing the operator to regulate the intake performance. These motors are housed in a robust casing, which includes a sound-absorbing sponge to ensure a reduced noise level is maintained.

The gathered liquid passes through a PPL filter with a 150µ efficiency, which enables the separation of even the tiniest solid particles. This process ensures that the filtered liquid becomes suitable for reuse. The filter is designed to be easily washed and reused. Additionally, there is an alternative disposable TNT filter with a 100µ efficiency that is also available.

The container of the vacuum cleaner is fitted with a bottom drain tube for the purpose of draining the collected liquid. The liquid is discharged from the container using the force of gravity.

An electric level probe immediatley stops suction when the liquid exceeds a certain container fill level, protecting the suction unit.
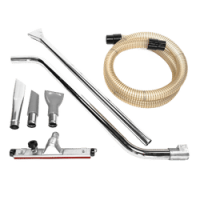
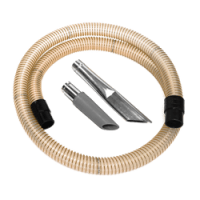
Get answers about using the M 130 OIL P for CNC sump cleaning, coolant and cutting-oil recovery, metal chip and swarf separation, liquid filtration, powered coolant discharge, coolant recovery workflows, and choosing the right sump vacuum for machine-tool maintenance.
The M 130 OIL P is a compact CNC sump vacuum designed to recover coolant or cutting oil together with metal chips, swarf, and other settled machining debris while providing powered liquid discharge.
Two independently controlled bypass motors provide up to 226 CFM of airflow and 94 inH2O of maximum vacuum through a 2-inch inlet. The machine operates on 115 V / 60 Hz single-phase power, making it practical for machine-side maintenance without requiring three-phase electrical service.
The M 130 OIL P provides 34 gallons of liquid capacity and 10 gallons of solids capacity. A sieve-grid basket separates larger chips and swarf from the recovered liquid, while a liquid-filtration stage can further reduce suspended contamination.
Its built-in submerged discharge pump makes the M 130 OIL P especially useful when recovered coolant needs to be transferred through a hose to another container, disposal point, treatment system, or back toward a machine after the coolant has been evaluated for reuse.
Yes. The M 130 OIL P is specifically designed for mixed liquid-and-solid recovery from CNC machine sumps, tanks, worktables, and other machine-tool areas.
Coolant or cutting oil can be recovered together with metal chips, swarf, and suitable settled machining debris during the same sump-cleaning process.
A sieve-grid basket separates larger chips and swarf from the recovered liquid before the liquid enters the main collection area. A liquid-filter option can then provide additional filtration of smaller suspended contamination.
This separation makes it easier to handle the recovered solids independently from the coolant or cutting oil instead of collecting the entire sump contents as one mixed waste stream.
The application should still be reviewed when the fluid contains unusually heavy sludge, extremely fine metallic particles, reactive substances, flammable liquids or vapors, hot fluids, or other hazardous contaminants.
The M 130 OIL P combines solid separation, liquid filtration, and powered discharge in one CNC sump-cleaning workflow.
During recovery, larger metal chips and swarf are retained in a removable sieve-grid basket while coolant or cutting oil continues into the liquid collection section.
A washable 150 µm liquid filter can be used to reduce smaller suspended solids. A disposable 100 µm TNT liquid filter is also available when a different filtration setup is preferred.
An electric level system protects the suction unit when the collection tank reaches its operating fill level.
Recovered liquid can then be transferred using the built-in submerged discharge pump. The current U.S. specification rates the pump at approximately 35.66 gallons per minute.
This separation and filtration can support coolant-recovery workflows, but it should not be treated as complete coolant conditioning. Coolant concentration, tramp oil, bacteria, fine particles, chemistry, and other process requirements should still be checked before recovered coolant is returned to a CNC machine.
Choose the M 130 OIL P when powered coolant transfer is an important part of the sump-cleaning workflow. Choose the M100 OIL when greater suction airflow and a simpler gravity-discharge process better fit the application.
The M 130 OIL P provides 34 gallons of liquid capacity and 10 gallons of solids capacity. It produces up to 226 CFM and 94 inH2O and includes a submerged discharge pump rated at approximately 35.66 gallons per minute.
The M100 OIL provides 26 gallons of liquid capacity and 13 gallons of solids capacity. It increases suction performance to 326 CFM and 98 inH2O but uses gravity as its standard liquid-discharge method.
The M 130 OIL P therefore provides more liquid capacity and powered transfer, while the M100 OIL provides more solids capacity and higher vacuum airflow.
Choose between them based on sump size, chip loading, required pickup performance, and whether recovered coolant needs to be pumped through a hose or can simply be drained by gravity.
The M 130 OIL P may not be the best choice when the application requires substantially more than 34 gallons of liquid recovery between emptying cycles, when chip loading exceeds its 10-gallon solids capacity, or when a higher-volume multi-machine maintenance workflow is required.
For smaller machine tanks where powered liquid discharge is unnecessary, a compact gravity-discharge sump vacuum may provide a simpler workflow.
For larger CNC sumps, repeated high-volume cleanouts, or maintenance routes covering multiple machines, a RAM OIL 200 MP, RAM OIL 280 MP, or larger RAM OIL system may provide greater recovery capacity.
The M 130 OIL P should also not automatically be assumed suitable for flammable liquids or vapors, reactive chemicals, hot fluids, unknown hazardous mixtures, or hazardous classified locations.
Final selection should consider sump volume, coolant volume, chip and sludge loading, fluid chemistry, temperature, flash point where applicable, hose run, required pickup rate, discharge destination, coolant-reuse requirements, and operating environment.