- (737) 320-9102


2.7 HP | 120V 1~

18 gal
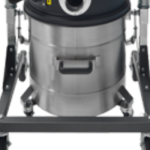
The M 70 OIL sump vacuum is a compact 120 V solution for CNC coolant tank cleaning, cutting-oil recovery, and the separation of metal chips and swarf. Two by-pass motors deliver up to 230 CFM airflow and 94 inH2O vacuum through a 2-inch inlet. A metal separation basket and 150 µm liquid filtration help separate chips and swarf from recovered liquid, while an electric high-level sensor stops suction when the collection tank reaches its maximum fill level.
With 18-gallon liquid capacity, 10-gallon solids capacity, wheeled mobility, and gravity discharge, the M 70 OIL is well suited to recurring machine-side cleanouts and smaller CNC sumps. An optional immersion pump is available for powered liquid discharge when required by the application.

Two independently switched by-pass motors deliver up to 230 CFM airflow and 94 inH2O vacuum, allowing the operator to run one or both motors to match the cleanout task.

A 150 µm liquid filter works with the metal separation basket to help separate chips and swarf from recovered coolant or cutting oil during sump and machine-tank cleanout.

Recovered liquid drains through the bottom outlet by gravity. An optional immersion pump is available for powered discharge when a faster pump-out workflow is required.

An electric level sensor stops suction when liquid reaches the preset maximum fill level, helping protect the suction unit from overfill during tank recovery.

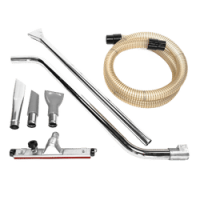
Get answers about using the M 70 OIL for CNC sump cleaning, coolant and cutting-oil recovery, metal chip and swarf separation, liquid filtration, gravity or powered discharge, and choosing the right sump vacuum for machine-tool maintenance.
The M 70 OIL is a compact sump vacuum designed for CNC coolant-tank cleaning, cutting-oil recovery, and the separation of metal chips, swarf, and settled solids from recovered liquid.
Two independently switched bypass motors provide up to 230 CFM of airflow and 94 inH2O of maximum vacuum through a 2-inch inlet. Its compact 120 V single-phase design makes it well suited to recurring machine-side maintenance where operators need to clean smaller CNC sumps without using a larger high-capacity recovery system.
The M 70 OIL provides 18 gallons of liquid capacity and 10 gallons of solids capacity. A metal separation basket and 150 µm liquid filter help separate chips and swarf from coolant or cutting oil during recovery.
It is a strong fit for smaller CNC machines, job shops, prototype facilities, and machine-tool maintenance routes where compact size, mobility, and straightforward coolant-and-chip separation are priorities.
The M 70 OIL is designed to recover coolant, cutting oil, metal chips, swarf, and settled solids commonly found in CNC machine sumps and machine-tool tanks.
During pickup, liquid and solid material enter the same recovery system. The metal separation basket captures larger chips and swarf while the liquid passes through a 150 µm filter before entering the collection tank.
This makes the M 70 OIL useful for machine tanks containing mixtures of coolant and machining debris rather than requiring operators to remove the liquid and chips in separate cleanup steps.
The exact application should still be reviewed when material includes unusually fine metallic particles, heavy sludge, abrasive solids, reactive materials, hot liquids, flammable liquids or vapors, or other hazardous contaminants. Those conditions may require a different vacuum, additional filtration, or a specialized recovery process.
The M 70 OIL uses a metal separation basket together with a 150 µm liquid filter to separate metal chips, swarf, and larger suspended solids from recovered coolant or cutting oil.
As the coolant-and-chip mixture enters the vacuum, larger solids remain in the separation basket while the liquid continues through the filtration stage into the collection tank. This makes the collected chips easier to remove separately and provides a cleaner recovered liquid stream than simply pumping the entire sump contents into one container.
Filtered coolant may be evaluated for reuse, but the M 70 OIL should not be treated as a complete coolant-conditioning system. A 150 µm filter removes bulk contamination but does not control coolant concentration, bacteria, tramp oil, dissolved contaminants, very fine particles, or other fluid-quality conditions.
Before recovered coolant is returned to a machine, its concentration, contamination level, odor, biological condition, tramp-oil content, and process requirements should be checked. Applications requiring finer filtration, coalescing, centrifuging, or full coolant conditioning may require additional equipment.
Choose the M 70 OIL when compact size and smaller CNC sump cleanouts are the priority. Choose the M100 OIL when the application requires greater liquid capacity, greater solids capacity, and higher pickup airflow.
The M 70 OIL provides an 18-gallon liquid capacity, 10-gallon solids capacity, up to 230 CFM airflow, and 94 inH2O maximum vacuum.
The M100 OIL increases liquid capacity to 26 gallons and solids capacity to 13 gallons while providing up to 326 CFM airflow and 98 inH2O maximum vacuum.
Both models are designed for coolant, cutting-oil, chip, and swarf recovery and use gravity as the standard liquid-discharge method.
The M 70 OIL is therefore a strong compact option for smaller machine tanks and routine machine-side maintenance, while the M100 OIL is the better step up when larger sumps, more chips, more recovered liquid, or higher pickup performance are required.
The M 70 OIL may not be the best choice when the machine sump contains more liquid or chips than its 18-gallon liquid and 10-gallon solids capacities can handle efficiently, when the application requires repeated high-volume tank cleanouts, or when powered liquid transfer is an important part of the workflow.
The standard M 70 OIL drains recovered liquid by gravity. An optional immersion pump can be added when powered discharge is needed, but applications centered around frequent pump-out, larger coolant volumes, or multiple-machine maintenance may be better served by a purpose-built pump-equipped model such as the M130 OIL P or a larger RAM OIL sump vacuum.
The M 70 OIL should also not automatically be assumed suitable for flammable liquids or vapors, reactive chemicals, hot fluids, unknown hazardous mixtures, or hazardous classified locations.
Final selection should consider the sump volume, amount and type of chips or sludge, fluid chemistry, temperature, flash point where applicable, hose length, required pickup rate, discharge workflow, coolant-reuse requirements, and operating environment.