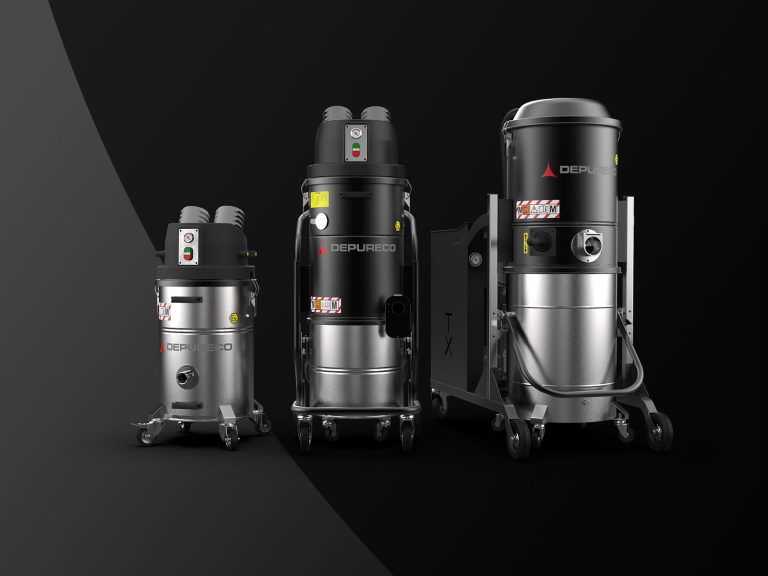
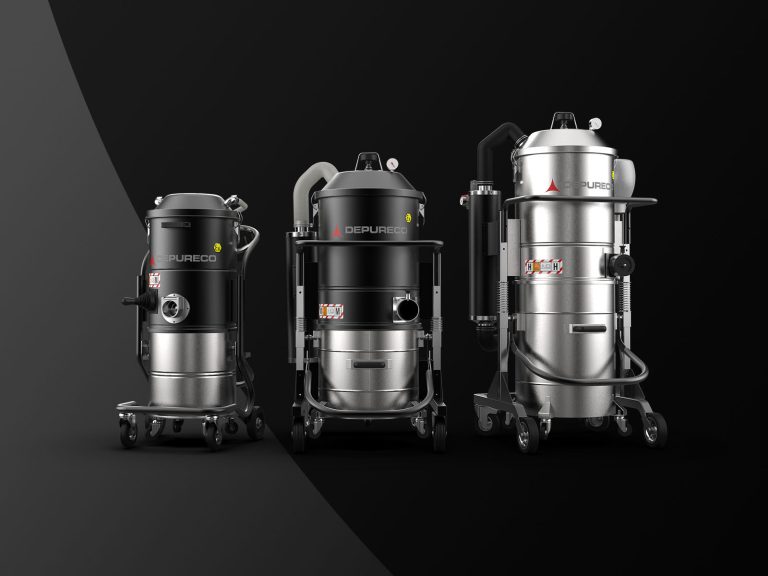
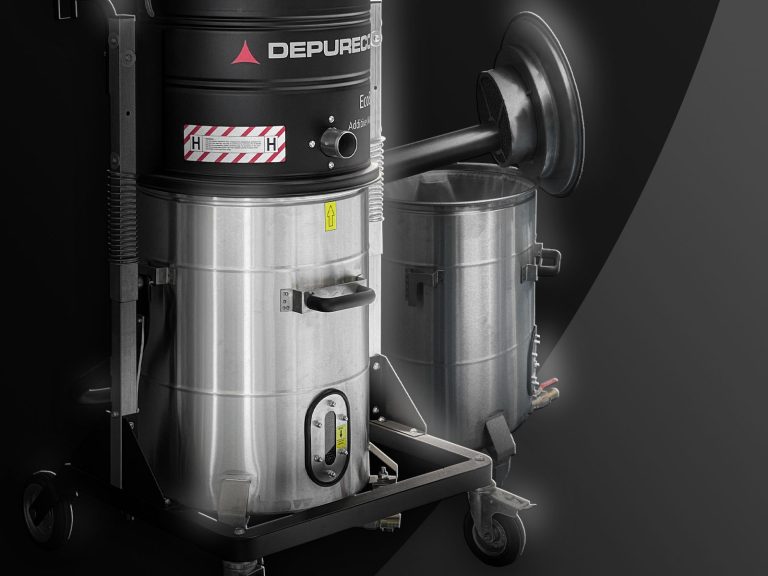
Compare industrial vacuum solutions for combustible dust, hazardous dust, conductive powders and reactive metal fines. Depureco USA offers ORD LOC housekeeping vacuums, air-powered systems, documented hazardous-area options and inertization configurations selected around the material, area classification and recovery process.
Best For: Facilities that need compact, mobile certified equipment for fine powders, dust accumulation, and high-risk cleanup tasks.
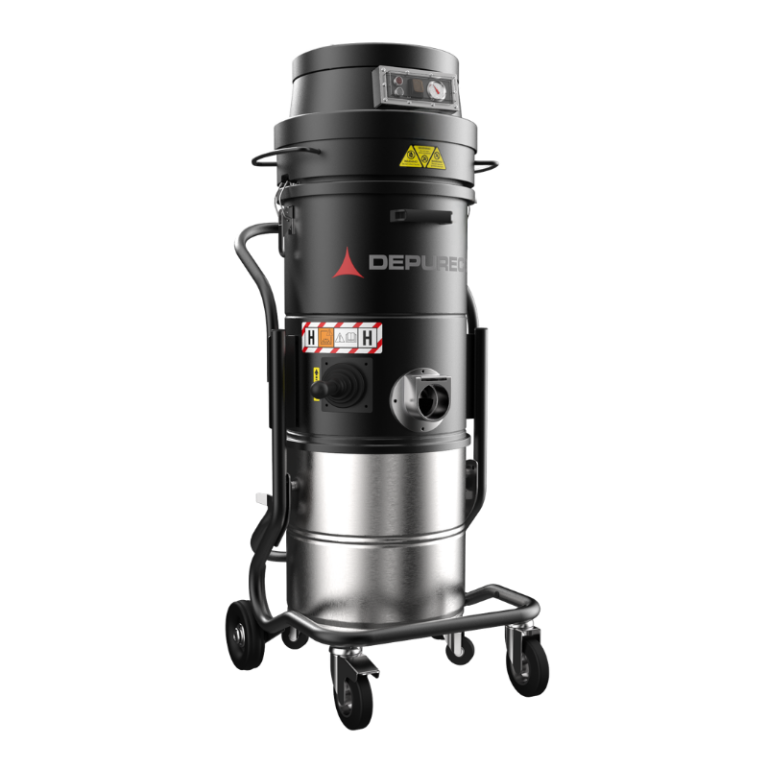
Brushless hazardous-dust vacuum for combustible dust and powder cleanup with antistatic Class M filtration, manual shaker cleaning, HEPA H14 filtration, grounding, and 12-gal stainless collection.
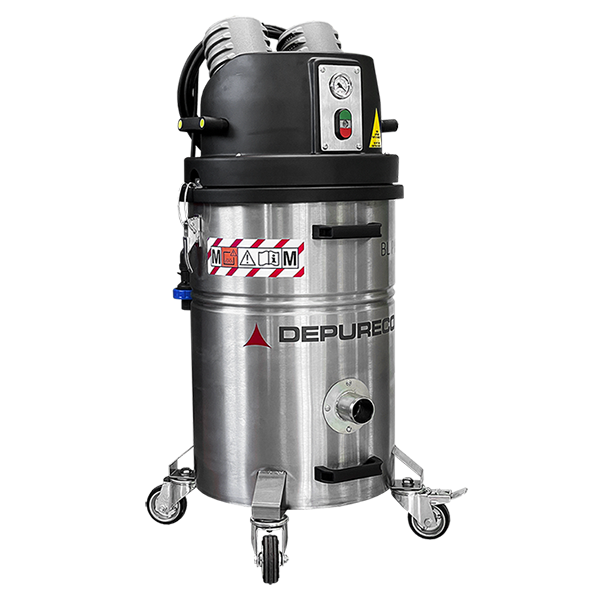
Compact brushless vacuum for hazardous dust and combustible powder cleanup with antistatic Class M filtration, HEPA H14 outlet filtration, grounded construction, and stainless collection.
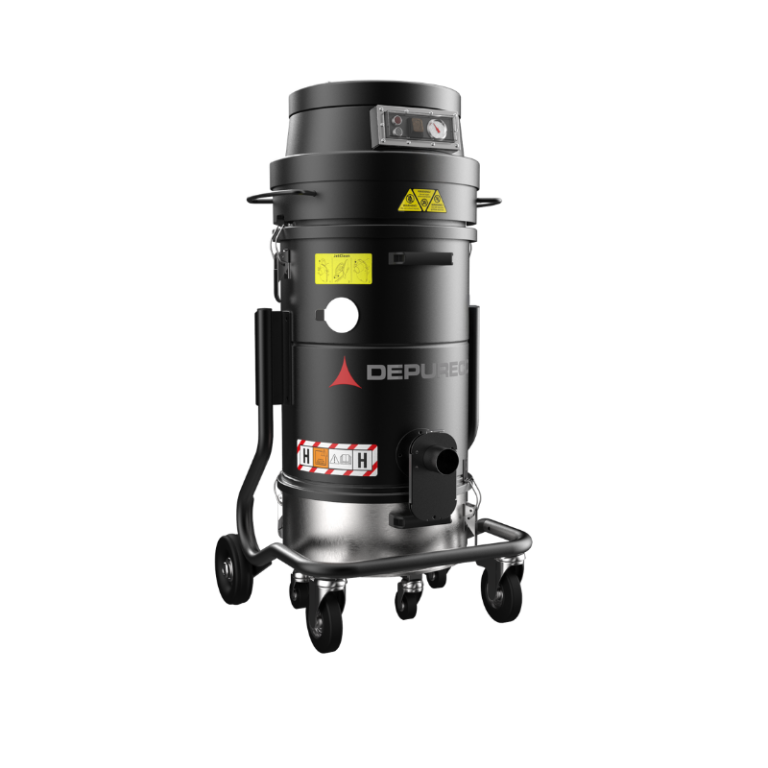
Compact brushless hazardous-dust vacuum with JetClean® cartridge cleaning, antistatic Class M filtration, HEPA H14 filtration, grounded construction, and stainless collection.
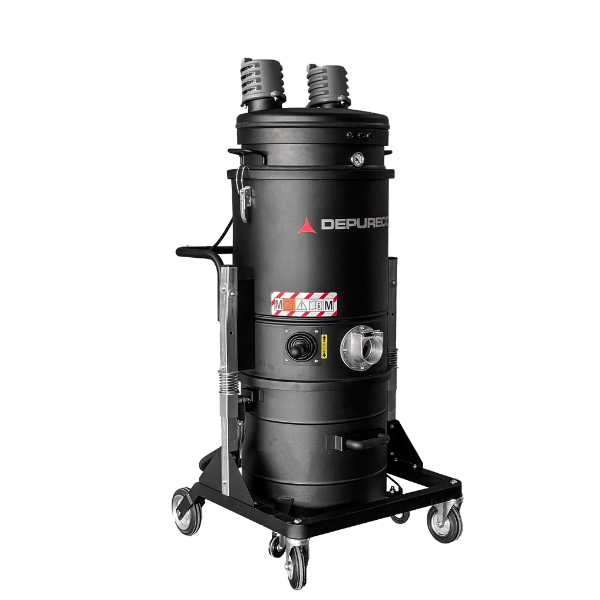
NFPA 660 compliant ordinary-location combustible dust vacuum with 3 by-pass motors, antistatic Class M filtration, manual shaker cleaning, and a 26-gallon bin.
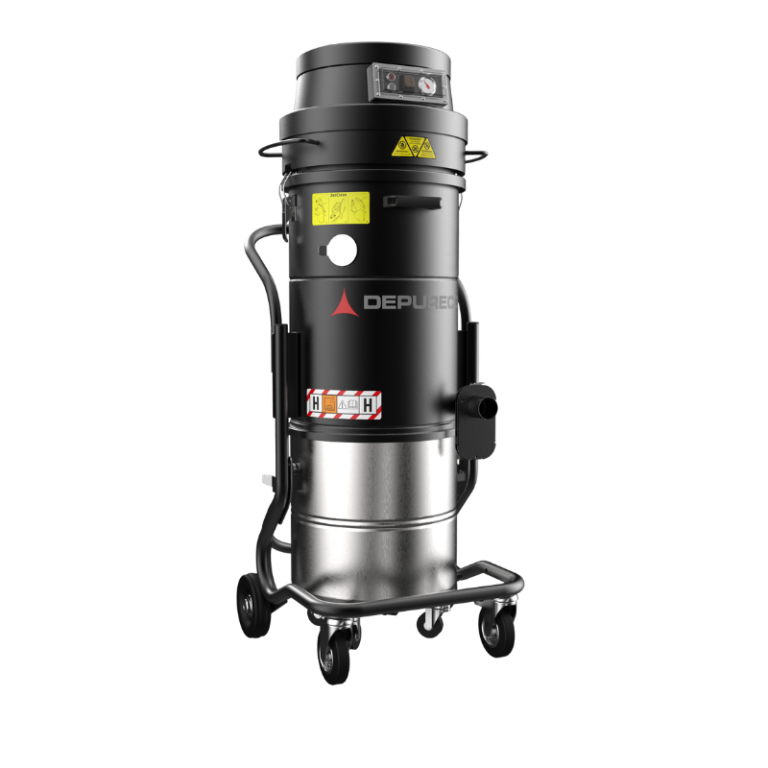
Brushless ORD LOC dust vacuum for combustible dust and powder cleanup with JetClean® cartridge cleaning, antistatic Class M filtration, HEPA H14 filtration, grounding, and 12-gal stainless collection.
Compressed-air vacuums for the most sensitive hazardous locations.
Best when facilities want non-electric recovery with continuous-duty performance and zero motor-based ignition risk at the point of use.
Best when facilities want non-electric recovery with continuous-duty performance and zero motor-based ignition risk at the point of use.
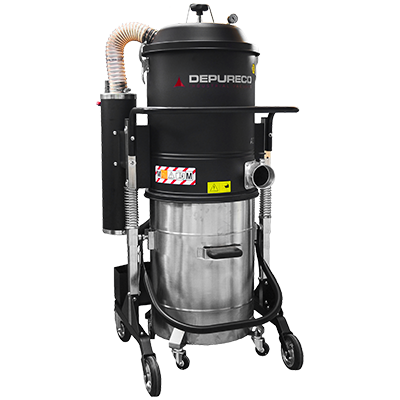
High-airflow pneumatic hazardous-dust vacuum with Venturi suction, antistatic M-Class filtration, grounding, manual filter cleaning, optional H14 filtration, and a 26-gal AISI 304 stainless steel collection bin.
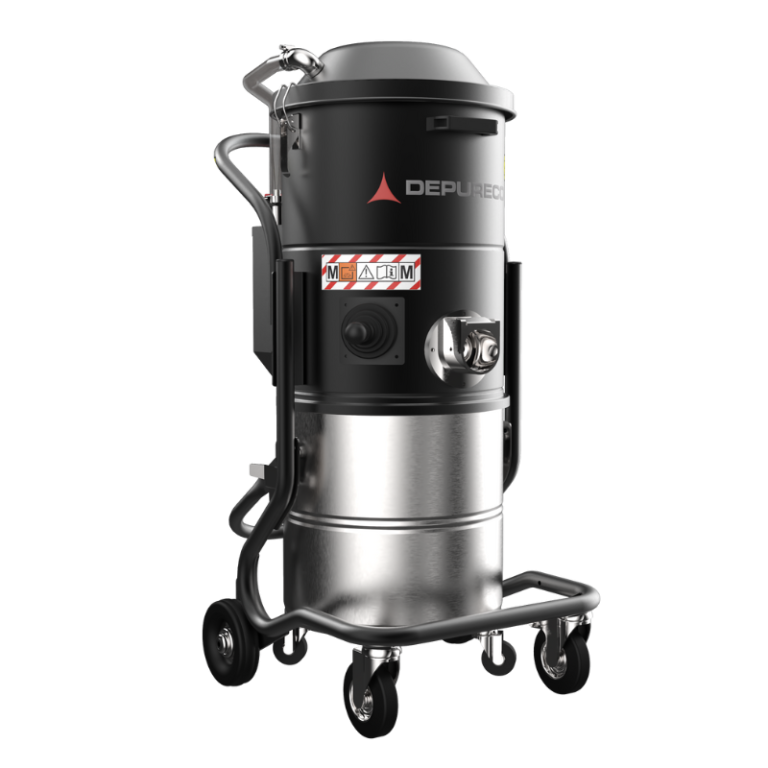
Compact pneumatic hazardous-zone vacuum with dual Venturi ejectors, antistatic Class M filtration, grounding, stainless collection, manual filter cleaning, and optional HEPA H14.
Inertization systems for the highest-risk metal powder recovery applications.
Designed for aluminum, titanium, magnesium, and other reactive conductive dusts where standard hazardous-dust recovery is not enough.
Best For: Explosive Metal Powders (Aluminum, Titanium, Magnesium). Neutralize the explosion risk immediately. Our inertization technology immerses collected dust in a liquid bath, instantly rendering it inert and safe for disposal.
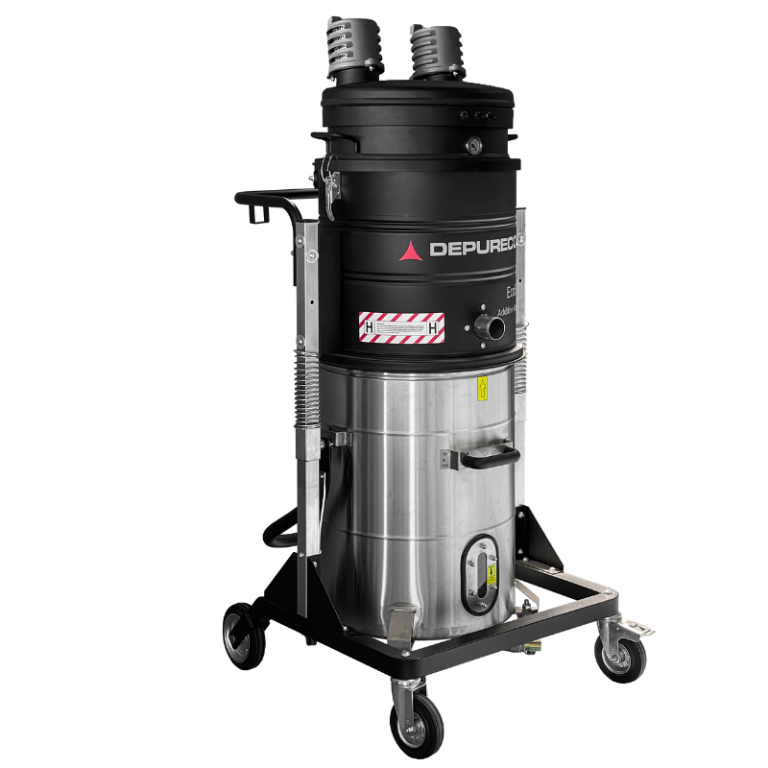
Metal powder vacuum for conductive dust and additive manufacturing powder recovery with 26-gal inert-liquid collection, complete grounding, hydrogen vent, and optional H14 filtration.

Brushless inerting vacuum for conductive metal powder recovery with liquid-bath collection, H13 antistatic filtration, stainless steel container, spark-trap protection, hydrogen venting, and 12-gallon capacity.

Explosion-proof vacuum selection starts with the environment, the material, and the cleanup task.
These systems are built for ignition-sensitive dust recovery where conductive accessories, grounding strategy, antistatic filtration, and certified equipment paths matter more than a standard industrial vacuum.
Not every dust cleanup job calls for the same vacuum category.
When the application involves classified areas, ignition-sensitive powders, conductive metal dust, or higher-risk particulate, the equipment path changes from general housekeeping to certified hazardous-area vacuum selection.


NFPA 660 helps frame the broader hazard context around combustible particulate, dust accumulation, and housekeeping practices.
On this page, the focus is not blanket compliance claims. It is selecting the right explosion-proof vacuum path when the application, the material, and the operating environment call for certified hazardous-area equipment.
Explosion-Proof” typically refers to electrical equipment contained within a heavy-duty housing designed to withstand an internal explosion without igniting the surrounding atmosphere.
“Intrinsically Safe” often refers to pneumatic (air-powered) vacuums that use no electricity and have no moving mechanical parts, thereby eliminating heat and sparks at the source.
Depureco USA offers both ATEX-certified electrical units and intrinsically safe pneumatic systems for Class I and Class II environments.
It depends on your hazard.
Class I is for flammable gases, vapors, and liquids (e.g., solvents, paint fumes).
Class II is for combustible dusts (e.g., flour, aluminum powder, wood dust).
Depureco USA specializes in Class II compliant vacuums engineered for NFPA 660 standards, ensuring safe recovery of volatile particulates.
Yes, in many specific applications.
ATEX is the rigorous European standard for explosive atmospheres. Equipment certified for ATEX Zone 22 is often engineered to meet or exceed the safety requirements for NFPA Class II, Division 2 environments.
Always verify with your local Authority Having Jurisdiction (AHJ), but Depureco’s ATEX-certified units provide a documented, third-party verified level of safety that standard “shop vacs” cannot match.
Pneumatic vacuums, like the Depureco Air-Powered Series, utilize a Venturi system to generate suction without electricity.
This makes them inherently safe for hazardous locations because they generate no heat and have no electrical motors that could spark.
They are the preferred choice for facilities with available compressed air lines looking for a maintenance-free, continuous-duty solution.
Unlike manual shaker systems that require the operator to stop work, Depureco’s JetClean® system uses a differential pressure sensor to trigger a powerful reverse jet of air automatically.
This cleans the filter during operation, maintaining peak suction and preventing dangerous dust accumulation on the filter media—a critical requirement for NFPA compliance.
Absolutely not.
Standard vacuums have internal motors where sparks can ignite conductive metal dust clouds, causing a violent explosion. You must use a specialized “Immersion Separator” or inertization vacuum.
Depureco’s inert systems immerse collected metal powder in a liquid bath (usually oil or water), instantly neutralizing the explosion risk by removing oxygen from the equation.
Yes.
All our explosion-proof and combustible dust vacuums come with a comprehensive technical dossier, including ATEX certificates, grounding continuity test results, and HEPA H14 filtration certificates.
This documentation is designed to support your Dust Hazard Analysis (DHA) and demonstrate due diligence to OSHA and fire marshals.
Using a standard shop vacuum for combustible dust is a severe safety violation and an explosion hazard. Standard commercial vacuums have three critical flaws that make them dangerous in hazardous environments:
Selection should begin with the material and operating conditions, not the vacuum model. Provide the material name and SDS, particle size, bulk density, estimated collection volume, pickup frequency, moisture condition, and any available Kst, Pmax, MIE, or resistivity data.
The application review should also identify whether the pickup area is ordinary or electrically classified, the available power or compressed-air supply, required hose length, duty cycle, filtration expectations, and how the collected material will be discharged or disposed of.
For reactive metals, mixed powders, flammable liquids, toxic dusts, or unknown materials, additional testing and written application review may be necessary before equipment is recommended.
Related links:
No. The presence of combustible dust does not, by itself, establish that the pickup area is a Class II classified location. A facility may have a combustible-dust hazard while performing housekeeping in an ordinary location, or it may have a defined Class II Division 1 or Division 2 area based on how frequently hazardous dust concentrations are expected to occur.
The required vacuum configuration depends on the facility’s dust hazard analysis, electrical area-classification documentation, process conditions, material characteristics, and authority having jurisdiction. An ORD LOC combustible-dust vacuum may support housekeeping outside a classified location, but it should not be represented as approved for a Class II location unless the complete equipment marking and documentation support that use.
Related links:
ORD LOC identifies equipment intended for ordinary-location applications rather than electrically classified hazardous locations. Class II Division 1 generally applies where combustible dust may be suspended in hazardous quantities during normal operation. Class II Division 2 generally applies where hazardous dust concentrations are not normally present but may occur because of abnormal conditions, or where accumulated dust can interfere with heat dissipation or ignition control.
ATEX Zone 21 and Zone 22 are European dust-zone classifications. Zone 21 addresses areas where an explosive dust atmosphere is likely to occur occasionally during normal operation. Zone 22 addresses areas where it is not likely during normal operation and, if it occurs, persists only briefly.
These systems are related but not automatically interchangeable. Equipment must be evaluated against the classification system, dust group, temperature requirements, markings, and approval rules governing the actual facility.
Related links:
Not automatically. ATEX certification documents suitability under the applicable European directive and Zone classification. A U.S. facility may instead require equipment approved or listed for a specific Class, Division, Group, Zone, temperature code, or protection method by an acceptable testing organization.
An ATEX marking should not be translated directly into a U.S. Class II Division 1 or Division 2 claim without a documented engineering and regulatory basis. Before approval, review the equipment label, certificate, test standard, dust group, temperature limitations, complete system configuration, and any requirements imposed by the authority having jurisdiction, insurer, engineering firm, or corporate EHS program.
Depureco USA should identify exactly which documentation accompanies the proposed configuration rather than describing all ATEX-marked equipment as universally accepted in the United States.
Related links:
A vacuum cannot make an entire facility, process, or housekeeping program NFPA 660 compliant. Vacuum selection is one part of a broader combustible-dust risk-management program that can include a dust hazard analysis, material testing, ignition-source control, electrical area classification, housekeeping procedures, training, inspection, maintenance, and management of change.
When a vacuum is described as supporting NFPA 660 housekeeping, the claim should refer to documented features such as grounding provisions, antistatic or conductive components, suitable filtration, dust containment, appropriate collection methods, and configuration for the intended ordinary or classified location.
The facility remains responsible for determining whether the complete installation and operating procedure satisfy its DHA, adopted codes, insurance requirements, and authority having jurisdiction.
Related links:
Review the documentation for the exact quoted configuration, not only a general product-family brochure. The approval package may need to include the product label, declaration or certificate, applicable test standards, Class, Division, Group, or Zone marking, temperature limitations, operating manual, grounding instructions, filter specifications, permitted accessories, maintenance requirements, and material limitations.
The documentation should also identify whether the vacuum is intended for ordinary locations, hazardous locations, ATEX zones, conductive dusts, reactive metal powders, or another defined application. Confirm that replacement filters, hoses, tools, collection bags, separators, and other components preserve the properties required by the application.
For high-risk applications, submit the complete package to the facility engineer, EHS team, authority having jurisdiction, insurer, or third-party dust consultant before purchase.
Related links:
No. Removing an onboard electric motor eliminates one potential electrical ignition source, but it does not automatically make the complete vacuum intrinsically safe or approved for every hazardous location.
The complete system still requires evaluation for static charge, grounding continuity, mechanical sparks, hot surfaces, conductive dust accumulation, material compatibility, filter construction, collection method, and the classification of the pickup area. The hose, couplings, floor tools, nozzles, separator, drum, and discharge components can be as important as the vacuum body.
Compressed-air pressure, available SCFM, operating cost, noise, and duty cycle also affect whether a pneumatic vacuum is practical. Use “intrinsically safe” only when the exact equipment documentation and approved protection method support that designation.
Related links:
No. A brushless motor can remove brush arcing associated with conventional brushed motors, but it does not independently establish that the complete vacuum is explosion-proof, dust-ignition-proof, intrinsically safe, or approved for a classified location.
Suitability depends on the complete design, including the motor and electrical components, surface temperatures, grounding path, filters, housing, seals, collection system, hose, accessories, mechanical construction, and product markings. A brushless ORD LOC vacuum may be appropriate for combustible-dust housekeeping outside a classified location without being approved for use inside a Class II area.
The correct question is not whether the motor is brushless. It is whether the complete documented configuration is suitable for the material, location classification, duty cycle, and collection method.
Related links:
Static control must extend through the complete material path. A grounded vacuum body does not provide adequate protection if the hose, couplings, wand, floor tool, separator, liner, or collection container interrupts electrical continuity.
Moving dry powder through a hose can generate electrostatic charge. Conductive or antistatic components provide a controlled path for that charge when they are correctly connected, maintained, and grounded. The required resistance and construction depend on the material, equipment design, and applicable safety strategy.
Inspect connections regularly and replace components with compatible parts. A nonconductive aftermarket hose or tool can undermine the intended configuration. Also distinguish ESD-safe equipment for electronics from equipment evaluated for combustible dust or a classified hazardous location; those designations address different risks.
Related links:
A conventional shop vacuum should not be selected for combustible-dust cleanup based only on suction power, a metal tank, a HEPA filter, or an aftermarket antistatic hose. Those features do not establish grounding continuity, ignition-source control, classified-location suitability, safe filter cleaning, or contained material discharge.
A suitable industrial configuration must be evaluated as a complete system for the actual dust and pickup location. Important factors include whether the area is ordinary or classified, the dust’s explosibility and conductivity, filtration, grounding, accessory construction, container design, filter-cleaning method, and operator exposure during emptying.
Consumer terminology such as “shop vac,” “HEPA shop vacuum,” or “stainless steel vacuum” should not be treated as an equipment rating for combustible-dust service.
Related links:
Do not select a metal-powder vacuum from the metal name alone. Identify the exact metal or alloy, particle-size distribution, moisture condition, production process, contamination risk, collection volume, and whether the material is dust, chips, fines, condensate, or additive-manufacturing powder.
Aluminum, magnesium, titanium, and their alloys can behave differently, and mixed-metal dust may introduce additional reactivity. The review should determine whether dry collection, wet collection, liquid immersion, inertization, dedicated equipment, or another engineered method is appropriate.
The selected configuration must also account for electrical area classification, conductivity, grounding, filtration, safe discharge, material reuse, and waste handling. Unknown or mixed metal powders should not be vacuumed until their properties and approved collection method are established.
Related links:
Inertization or liquid-immersion collection may be considered when dry recovery would allow reactive metal powder to accumulate in an unsafe condition. The correct method depends on the specific metal or alloy, particle size, contamination, process history, reactivity data, approved liquid or inert medium, and disposal or recycling procedure.
Water, oil, and other liquids are not universally interchangeable. A liquid that is appropriate for one powder may react with another material, interfere with downstream recycling, or create a separate disposal hazard. The collection medium, fill level, inspection procedure, discharge method, and change-out interval must follow the approved equipment and material-handling procedure.
The facility should establish the collection method before selecting the vacuum, not after the powder has already entered the machine.
Related links:
There is no single “bakery dust rating.” Selection depends on the exact ingredient, particle size, explosibility data, accumulation rate, sanitation requirements, pickup location, and electrical area classification.
The application review should determine whether the vacuum will collect floor accumulation, clean mixers or packaging equipment, reach overhead structures, recover spilled ingredients, or support frequent changeovers. It should also address cross-contact, allergen control, food-contact expectations, stainless-steel construction, conductive accessories, filtration, contained discharge, and whether equipment must be dedicated to one ingredient or production area.
A facility with combustible organic dust may need an ORD LOC housekeeping vacuum, hazardous-location equipment, or a centralized system depending on the DHA and area classification.
Related links:
First determine whether the collected powder will be discarded or returned to the coating process. Reclaim applications require tighter control of color contamination, foreign material, filter shedding, and contact surfaces than general booth housekeeping.
The powder chemistry, SDS, particle characteristics, combustibility, area classification, collection volume, and cleaning frequency should be reviewed before selecting the vacuum. The complete pickup system may require conductive hoses and tools, grounding continuity, suitable filtration, controlled filter cleaning, and a discharge method that minimizes airborne powder.
Do not assume that equipment used outside a spray booth is appropriate inside a classified booth or powder-handling area. The location and task should be evaluated separately, even when the same coating powder is involved.
Related links:
“Explosion-proof” should not be interpreted as blanket authorization to recover every liquid. The liquid identity, flash point, vapor pressure, chemical compatibility, temperature, contamination, pickup volume, and area classification must be evaluated against the vacuum’s documentation.
Some applications involve a combustible-dust hazard, while others involve flammable gases or vapors governed by a different classification. Equipment suitable for a dust-classified area is not automatically suitable for a Class I vapor hazard. The motor or power source is also only one part of the system; seals, hoses, filters, container materials, grounding, discharge, and vapor management must be considered.
Provide the SDS and operating conditions before attempting to collect solvents, fuels, reactive liquids, or unknown chemical mixtures.
Related links:
No. HEPA classification addresses particulate filtration efficiency. It does not establish static control, explosion protection, dust-ignition protection, classified-location approval, or compatibility with a reactive material.
A hazardous-dust configuration may combine antistatic or conductive primary filtration with an H13 or H14 final filter to improve containment of fine or toxic particulate. However, the complete system must still be evaluated for grounding, ignition sources, surface temperatures, filter cleaning, collection, discharge, accessories, and area classification.
Filter placement also matters. A final HEPA filter can provide secondary containment, but it should not be used to compensate for an undersized primary filter or an unsuitable dust-handling design.
Related links:
Fine powder can blind a filter long before the collection container is full. A larger filter area reduces air velocity through the media and can extend the interval between cleaning, but performance also depends on dust characteristics, moisture, pickup rate, hose configuration, and the cleaning mechanism.
Manual shakers are practical for intermittent housekeeping when operators can stop and clean the filter. JetClean, reverse-jet, or automatic pulse-cleaning systems are better suited to applications where filter loading is rapid or interruptions are expensive. Some continuous processes also require redundant filtration, pre-separation, automatic discharge, or a three-phase continuous-duty vacuum source.
Sizing should be based on expected loading over the shift, not clean-filter airflow measured at the beginning of the job.
Related links:
Airflow and vacuum pressure serve different functions. Airflow carries suspended dust and light material through the hose, while vacuum pressure helps move dense material, overcome restrictions, and maintain pickup over longer or more demanding hose runs.
Sizing should account for material density, particle size, desired pickup rate, hose diameter, horizontal distance, vertical lift, number of bends, floor-tool width, simultaneous operators, filter loading, and the difference between intermittent and continuous operation. Container capacity should reflect how much material can be handled safely before emptying, not simply the largest bin available.
A cyclone or pre-separator may be more effective than selecting a larger vacuum when the application involves high volumes, abrasive material, reusable product, or rapid filter loading.
Related links:
Use a portable industrial vacuum for point cleanup, maintenance tasks, spill recovery, machine cleaning, and applications that move between production areas. Consider a centralized vacuum system when multiple operators, fixed pickup points, long hose runs, overhead cleaning, or facility-wide housekeeping create repeated demand.
A dust collector serves a different purpose. It is generally designed for source capture of airborne dust generated by a process, while an industrial vacuum recovers settled material, spills, accumulations, and process waste through a hose or fixed pickup point.
Some facilities need all three: source-capture dust collectors, a central housekeeping system, and portable vacuums for maintenance or isolated areas. Each component must still be evaluated for the dust and location classification.
Related links:
Start with documented application suitability, not review scores or advertised horsepower. Compare the exact location marking, permitted dust group or Zone, temperature limitations, electric or pneumatic drive, grounding continuity, conductive accessories, primary and final filtration, filter-cleaning method, collection system, duty-cycle rating, capacity, and discharge procedure.
Then compare the evidence supporting those claims: product labels, declarations, certificates, manuals, data sheets, test videos, and written application recommendations. Customer reviews can provide useful information about mobility, usability, service, noise, maintenance, and parts availability, but they do not establish compliance or suitability for a classified location.
Commercial comparison should also include required accessories, replacement-filter cost, consumables, warranty, U.S. parts availability, lead time, technical support, and whether material testing is available before purchase.
Related links: